Table of Contents
In advanced fields such as food technology, pharmaceuticals, new materials, and biotechnology, the precision of material processing during the laboratory stage directly influences the success of further research and industrial commercialization.
How to achieve particle size reduction from the micron scale to the nanoscale while maintaining high active ingredient retention and batch-to-batch consistency has become a critical challenge for researchers and process development engineers.
As an innovative company specializing in high pressure microfluidic homogenizers, JUNJIE develops advanced laboratory nano homogenizer solutions by combining extensive technical expertise with a deep understanding of laboratory research requirements. Our high-precision nano homogenization systems provide efficient, reliable, and repeatable processing solutions for scientific research, material development, and industrial applications.
Key Challenges in Laboratory Material Processing
During conventional laboratory material processing, researchers often face several challenges:
| Challenge | Description |
|---|---|
| Insufficient Particle Size Control | Traditional mixing equipment and colloid mills often struggle to achieve uniform nanoscale dispersion (<100 nm), limiting product performance and stability. |
| High Loss of Valuable Samples | Laboratory samples such as liposomes, vaccines, active proteins, and valuable plant extracts are often limited in quantity and high in value. Conventional equipment usually requires large processing volumes, resulting in material waste. |
| Poor Batch Reproducibility | Manual operation or unstable processing pressure can cause variations in particle size distribution and uniformity between batches, affecting research reliability. |
| Loss of Heat-Sensitive Components | Traditional homogenization processes generate significant heat, which may degrade heat-sensitive active ingredients such as vitamins, enzymes, and peptides. |
JUNJIE Laboratory Nano Homogenizer: Precision Breakthrough for Research
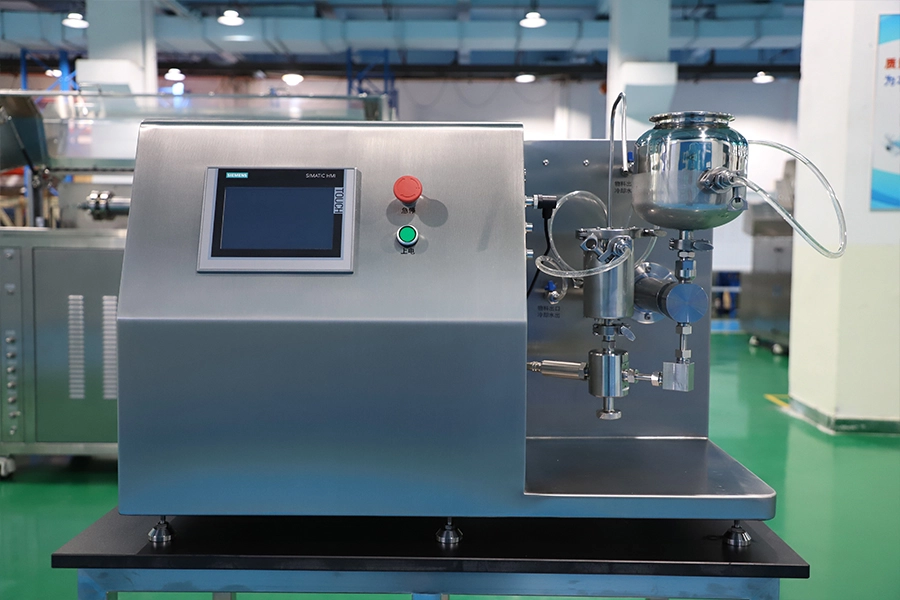
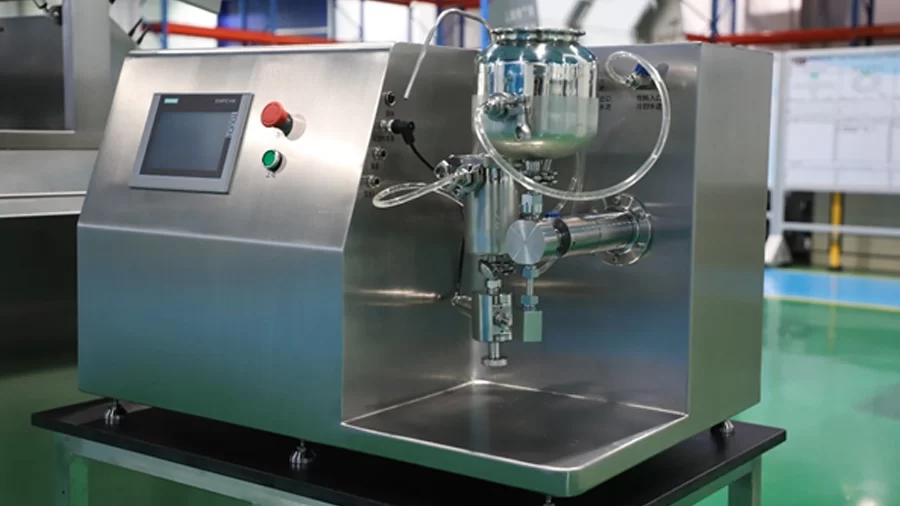
The JUNJIE laboratory nano homogenizer is specifically designed to address these laboratory challenges.
Based on advanced high pressure microfluidization technology, JUNJIE redefines laboratory homogenization accuracy by providing precise particle size control, minimal sample consumption, and highly repeatable processing performance.
Core Technology Principle
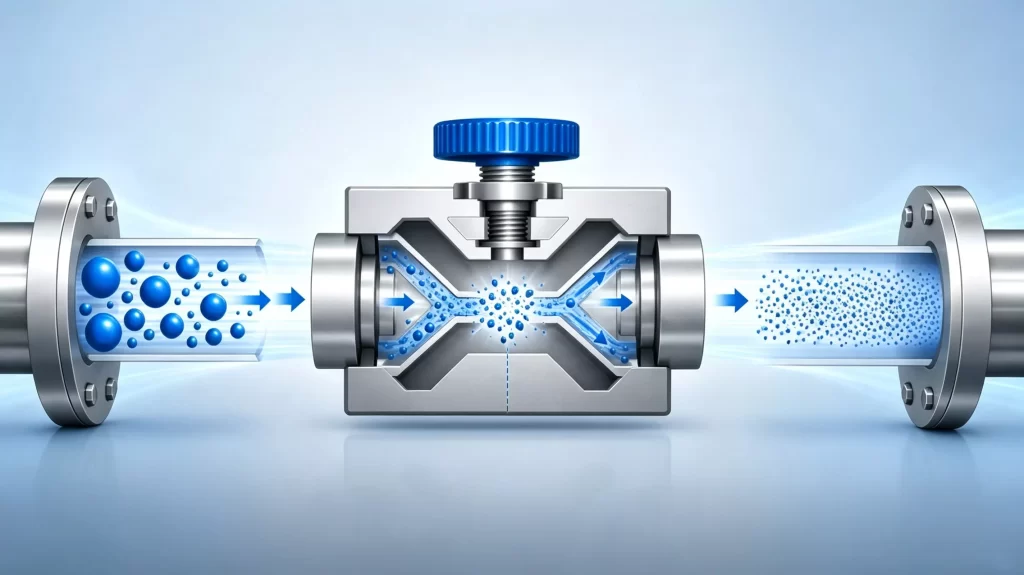
Based on high pressure microfluidization technology, materials are accelerated through a specially designed diamond interaction chamber under pressures up to 420 MPa.
During this process, materials experience intense physical effects including:
- High shear forces
- Particle collision
- Cavitation effects
These mechanisms enable efficient particle size reduction from the micron scale to the nanoscale while achieving highly uniform dispersion.
Core Advantages of JUNJIE Laboratory Nano Homogenizer
Designed for research applications requiring extremely fine particle control and high active ingredient preservation, JUNJIE laboratory nano homogenizers combine three key technologies:
- Micro-volume processing
- Precise pressure control
- Low-temperature homogenization
Together, these technologies provide a reliable, efficient, and repeatable solution for laboratory-scale nanoparticle dispersion and nano emulsification.
Micro-Volume Processing for Valuable Samples with Minimal Waste
Minimum Processing Volume as Low as 20 mL
Designed specifically for precious laboratory samples, JUNJIE nano homogenizers can process small-volume materials including:
- Liposomes
- Vaccine adjuvants
- High-value botanical extracts
This significantly reduces sample consumption and lowers research trial costs.
Servo Electric Cylinder Drive System
The servo electric cylinder provides stable and precise power output, avoiding pressure fluctuations commonly associated with traditional hydraulic systems during low-volume processing.
This ensures consistent and reliable experimental results.
Nanoscale Homogenization with Precise Particle Control
Efficient Dispersion and Particle Size Reduction
Through the powerful energy generated by high pressure microfluidization, JUNJIE systems enable uniform nanoscale dispersion with narrow particle size distribution.
Benefits include:
- Improved formulation stability
- Enhanced material performance
- Better bioavailability for applicable formulations
Precise Pressure Control
Equipped with high-precision pressure sensors and intelligent control systems, JUNJIE homogenizers maintain stable pressure conditions to ensure excellent batch-to-batch consistency.
Gentle Processing for Maximum Active Ingredient Preservation
Low-Temperature Homogenization
Unlike conventional thermal processing or high-shear methods, high pressure microfluidization can achieve efficient homogenization under controlled temperature conditions.
This helps preserve heat-sensitive components including:
- Vitamins
- Proteins
- Polyphenols
- Enzymes
while maintaining their functional properties.
Clean Label Processing
The process relies on physical treatment without chemical additives, supporting natural and clean-label product development concepts.
Intelligent Operation with Full Data Traceability
High-Resolution Touchscreen Control
The intuitive touchscreen interface allows users to easily set and store multiple processing parameters, including:
- Pressure
- Number of passes
- Processing conditions
This simplifies laboratory workflows and improves operational efficiency.
Data Recording and Process Traceability
The system automatically records key processing parameters, including:
- Pressure curves
- Temperature
- Processing time
Data can be exported and traced to support GLP (Good Laboratory Practice) requirements.
Typical Applications of Laboratory Nano Homogenizers
With outstanding performance and flexibility, JUNJIE laboratory nano homogenizers are widely used across multiple advanced industries.
Biopharmaceutical Applications
Used for particle size control and homogenization of:
- Liposomes
- Nanoemulsions
- Vaccine formulations
Helping improve:
- Encapsulation efficiency
- Formulation stability
- Targeted delivery performance
Food and Beverage Applications
Used for preparing:
- Plant-based emulsions
- Functional ingredients
- Nano-sized active compounds such as curcumin and Coenzyme Q10
Helping improve:
- Product texture
- Dispersion stability
- Ingredient absorption performance
Advanced Materials Applications
Used for nanoscale dispersion of:
- Graphene
- Carbon nanotubes
- Ceramic powders
Providing improved material uniformity and supporting the development of advanced material properties.
Cosmetics and Personal Care Applications
Used for developing:
- Nano active ingredient emulsions
- Advanced skincare formulations
- Functional serums
Helping enhance:
- Active ingredient delivery
- Product texture
- Formulation stability
Chemical Engineering Applications
Used for:
- Polymer dispersion
- Nano-scale emulsification
- Advanced chemical formulation development
Why Choose JUNJIE Laboratory Nano Homogenizer?
Among various laboratory nano homogenizer manufacturers, JUNJIE stands out through its deep understanding of laboratory research requirements and precise application-focused solutions.
JUNJIE provides more than a piece of equipment — it delivers a complete research toolchain covering process validation, optimization, and data management.
| Selection Advantage | Value Provided by JUNJIE |
|---|---|
| Advanced Technology | Years of R&D experience in high pressure microfluidization technology, enabling precise nanoscale particle reduction and uniform dispersion. |
| Technical Support | Free sample testing service allows customers to send materials for process evaluation before equipment investment. |
| Process Database | Supported by a database covering more than 1,000 material processing applications, enabling faster process matching and optimization. |
| Complete Service | Provides integrated support from process testing and equipment selection to installation and operator training. |
| Quality Assurance | Equipment manufactured under strict quality management systems with certifications including ISO9001 and ASME-U. |
Conclusion
In today’s rapidly evolving technology landscape, a high-performance laboratory nano homogenizer is more than a research tool — it is a key platform for overcoming processing challenges, accelerating innovation, and transforming laboratory discoveries into practical applications.
With four core advantages:
- Precise micro-volume processing
- Nanoscale homogenization
- Gentle active ingredient preservation
- Intelligent process control
JUNJIE laboratory nano homogenizers provide researchers with a reliable foundation from concept validation to process scale-up.
By combining high pressure microfluidization technology, advanced microfluidic homogenizer design, and comprehensive technical support, JUNJIE helps researchers and industries achieve more efficient and precise material processing.
Partner with JUNJIE and unlock the future of advanced homogenization technology.